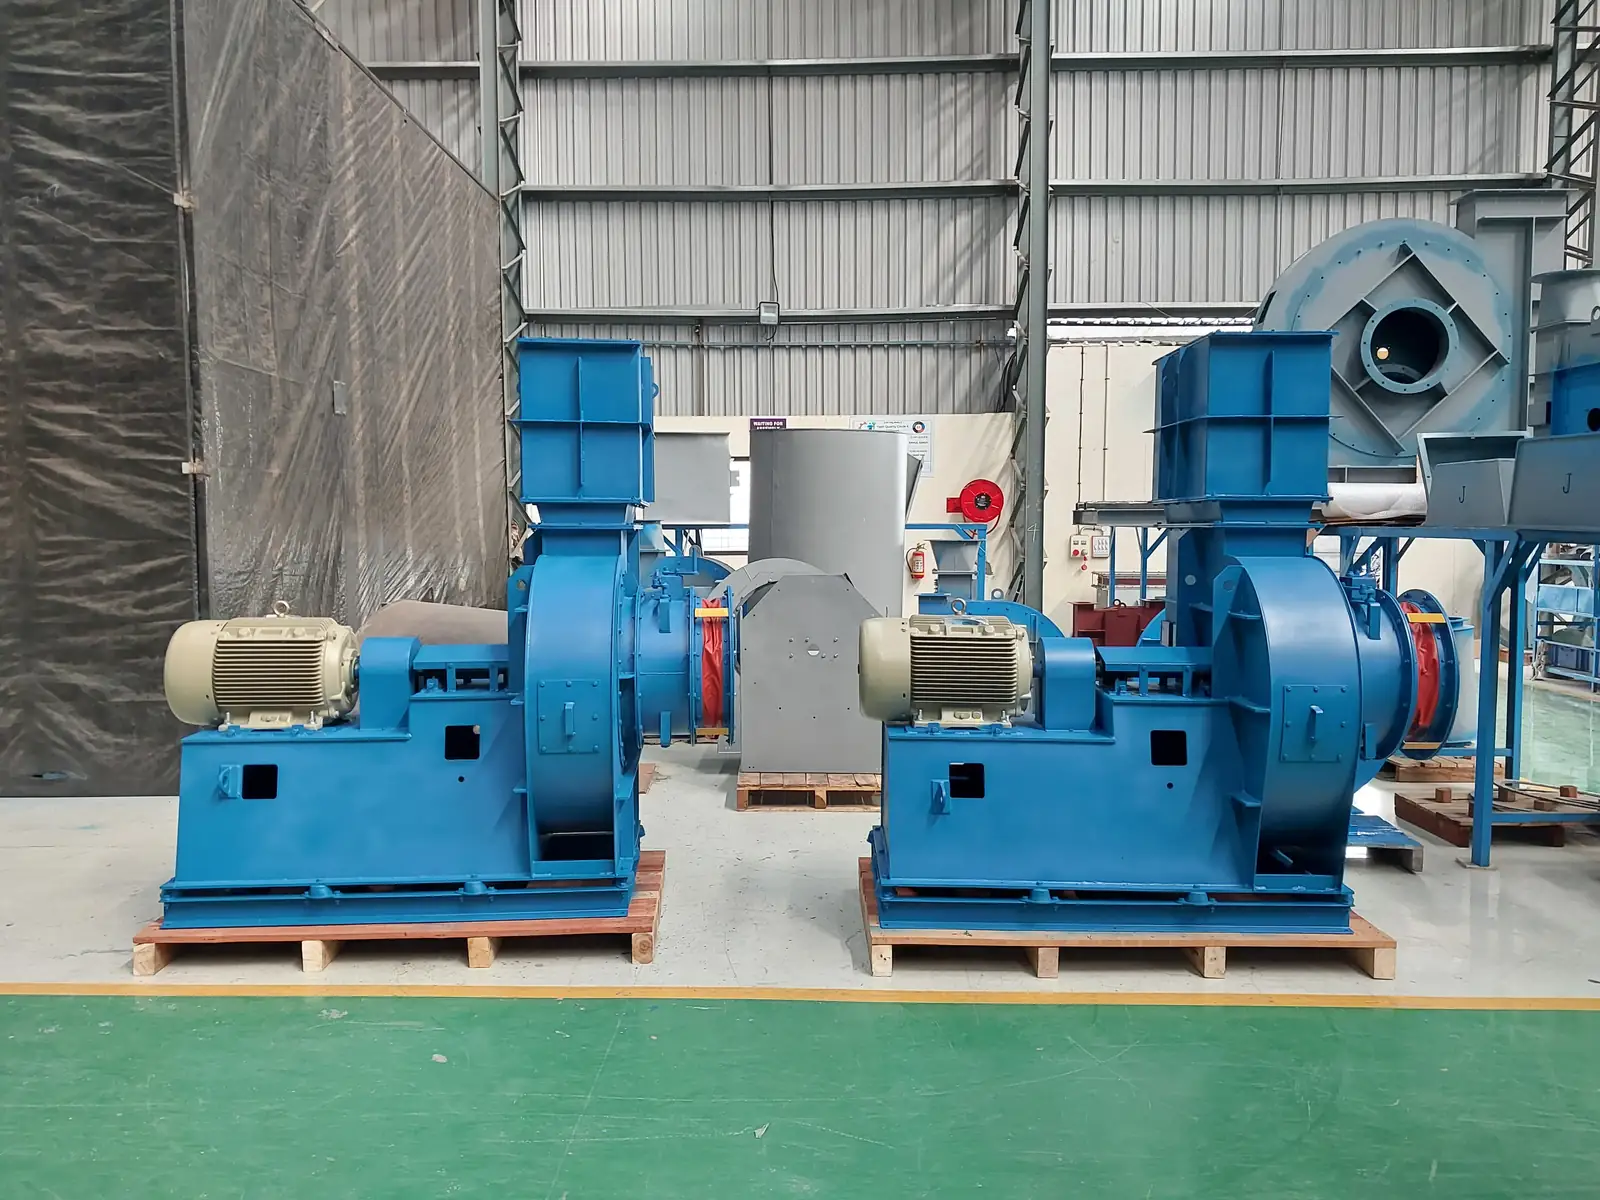
Two coupled-drive centrifugal fans on the Jitamitra shop floor
Home  /  Industries  /  Chemicals & Petrochemicals
Industries

Fans for chemical & petrochemical plants — where corrosion and ATEX are the norm.

A chemical or petrochemical plant asks the fan two hard questions at once: what is in the gas, and where does it run. The gas is corrosive — acid vapour, chlorides, solvent, wet scrubber carry-over — and the area is often classified hazardous, so the fan has to be built in the right alloy and to an ATEX construction at the same time. Fired-heater and process-boiler draught, corrosive and hazardous-area exhaust, FGD and scrubber boosters, reactor and solvent vents — each is a different chemistry. We engineer to the gas analysis and the area classification, not a catalogue near-fit: 908 chemical & petrochemical fans delivered, across the full envelope below — up to 2,25,000 CMH, 2,000 mmWC, 425 HP and 500 °C.

908chem & petrochem fans delivered
ATEX 2/22self-declared, Cat 3
316L / Duplexcorrosion metallurgy
2,000 mmWCmax static
In short

What fans are used in a chemical or petrochemical plant?

A chemical plant asks two questions at once: what is in the gas, and where does the fan stand. The gas is corrosive - acid vapour, chlorides, solvent, wet-scrubber carry-over - so the wetted parts are SS 304L, 316L, 310, 321 or Duplex 2205, or carbon steel coated over a Sa 2.5 blast. The area is often classified, so construction is spark-resistant with a motor to your stated zone, self-declared to ATEX Category 3 for Zone 2 and Zone 22.

15,000+
fans built since 2011
200 HP
VFD test rig · IS 4894 / AMCA 210
95%
on-time delivery (ERP statistics)
3–5
working days to quote

908 fans into Chemicals & Petrochemicals, across 36 customers — part of 15,000+ fans built since 2011.

FIRED-HEATER DRAUGHT · CORROSIVE EXHAUST · SCRUBBER BOOSTER · REACTOR & SOLVENT VENT · ATEX AREA
From our gallery

Fans we have built for chemical and petrochemical plants

Backward-curved plate fan built by Jitamitra for vacuum and exhauster duty, 170 CMH at 500 mmWC and 70 °C
170CMH/500mmWC/70°C
Vacuum / exhauster duty · Chemicals & Petrochemicals
Radial fan built by Jitamitra for pneumatic conveying in chemical and petrochemical plants, 650 CMH at 210 mmWC and 80 °C
650CMH/210mmWC/80°C
Pneumatic conveying (dilute) · Chemicals & Petrochemicals
Backward-curved fan built by Jitamitra for corrosive gas exhaust in chemical and petrochemical plants, 25,500 CMH at 150 mmWC
25,500CMH/150mmWC
Corrosive gas exhaust · Chemicals & Petrochemicals
Backward-flat plate fan built by Jitamitra for combustion and process air, 800 CMH at 475 mmWC and 40 °C
800CMH/475mmWC/40°C
Combustion / process air blower · Chemicals & Petrochemicals
Large backward-curved fan built by Jitamitra for corrosive gas exhaust, 1,020 CMH at 450 mmWC and 100 °C
1,020CMH/450mmWC/100°C
Corrosive gas exhaust · Chemicals & Petrochemicals
Centrifugal fan built by Jitamitra in chemical and petrochemical plants
Duty on request
Chemicals & Petrochemicals

See every build for chemical and petrochemical plants →

Where the fans sit

One plant, three jobs the fans have to do — and each one has its own chemistry.

Across a chemical or petrochemical plant the fans do three distinct jobs: they draught the fired heaters and process boilers, they exhaust corrosive and hazardous vapour from reactors, vents and scrubbers, and they boost the FGD and wet-scrubber circuits. Every one of them meets a defined gas chemistry and, more often than not, a classified hazardous area — so the fan is engineered to the gas analysis and the ATEX zone together, not to a duty point alone.

The duties we run in a chemical plant

The fan duties across a chemical or petrochemical plant — and the role each one plays.

A single process train needs a family of fan duties, from the clean, higher-pressure fired-heater FD to the wet, acid-laden scrubber booster. We have delivered 908 chemical & petrochemical fans across this list — each engineered to its own gas analysis, temperature and area classification, not adapted from a catalogue near-fit.

The fans we deploy here

Three fan types cover the chemical flowsheet — matched to the chemistry and the pressure.

The wheel is chosen by the gas and the pressure it has to make: a backward-curved plate for the clean, higher-efficiency fired-heater and process-air duty, an aerofoil where the gas is clean and the priority is efficiency, and a rugged radial for the wet, corrosive scrubber and dirty-side exhaust. All three build in the metallurgy the chemistry demands, and to an ATEX construction where the area calls for it — across the same envelope, to 2,25,000 CMH, 2,000 mmWC, 425 HP and 500 °C.

Why chemical fan duty is hard

Three things in chemical plant gas decide whether the fan lasts a turnaround or a season.

Chemical and petrochemical duty attacks a fan in three ways that a cement or power fan never sees — a corrosive chemistry that eats the wrong alloy, a classified hazardous area where a spark is a fatality, and a wet, saturated scrubber gas that condenses acid on every surface. Engineer for all three and the fan runs a full 3–5-year turnaround cycle between overhauls. Engineer for the duty point alone and it corrodes through, or worse, becomes the ignition source, within 6–18 months.

01 — CORROSION

Corrosive process chemistry

Acid vapour, chlorides, wet solvent and scrubber carry-over attack a mild-steel fan from the inside — pitting the wheel, thinning the casing, and unbalancing the rotor. The wrong alloy for the gas is eaten through within a single season, not a campaign.

How we engineer it out

Metallurgy sized to the gas analysis — 316L, Corten or Duplex 2205 on the wetted surfaces where chlorides and acids demand it — with a coating or FRP lining option, and the material chosen from your stated acid, chloride and moisture figures, not a default.

02 — IGNITION

Hazardous-area ignition risk

In a classified area the fan handles flammable solvent vapour, so a rub, a static discharge or a hot bearing is an ignition source. A standard fan is not built to keep every internal surface below the vapour's ignition energy.

How we engineer it out

An ATEX construction for Zone 2/22, Category 3 per 2014/34/EU (self-declared) — non-sparking wheel-to-casing clearances and material pairing, bonded and earthed rotor, and bearings kept cool and monitored, built spark-safe to the gas group and temperature class your area classification specifies, to keep internal surfaces below that stated temperature class.

03 — DEW POINT

Acid dew-point on wet gas

FGD and wet-scrubber gas leaves the absorber saturated and at the acid dew point (~120–150 °C), so acid condenses on the casing wall and the wheel and eats the metal — the booster fan sees the most aggressive condensate in the plant.

How we engineer it out

Corrosion-resistant metallurgy on the wetted surfaces, casing insulation and heat tracing to hold the wall above dew point, and drains at the low points — the dew-point margin sized to your SO₂/SO₃, chloride and moisture, so the condensate has nowhere to sit.

Jitamitra engineering resources
How we design for the plant

Every metallurgy, ATEX and dew-point choice is documented on the GA drawing you sign off — before we cut metal.

We don't sell a catalogue near-fit onto a chemical plant. Each fan is engineered to its own duty — the fired-heater FD to its clean pressure, the corrosive exhaust to its chemistry, the scrubber booster to its wet acid gas — at your operating point and your area classification.

  • Corrosion metallurgy to the gas — Material selected from your gas analysis — 316L, Corten or Duplex 2205 on the wetted surfaces where acid vapour and chlorides demand it, with coating or FRP-lining options — not a default alloy, so the wheel and casing survive the chemistry they actually see.
  • ATEX hazardous-area construction — ATEX Zone 2/22, Category 3 per 2014/34/EU (self-declared) where the area is classified — non-sparking clearances and material pairing, a bonded and earthed rotor, and bearings kept outside the airstream and monitored, built spark-safe to the ATEX zone, gas group and temperature class your area classification specifies, to keep internal surfaces below that stated temperature class.
  • Dew-point & wet-gas scope — For FGD, scrubber-booster and cooler exhaust below the acid dew point (~120–150 °C): corrosion-resistant wetted surfaces, casing insulation and heat tracing to hold the wall above dew point, and drains at the low points — the margin sized to your SO₂/SO₃, chloride and moisture.
  • Single source across the plant — One engineering partner for the whole flowsheet — fired-heater draught, corrosive and hazardous-area exhaust, scrubber boosters and process-air blowers — with 908 chemical & petrochemical fans delivered, so the fans, metallurgy and drives carry one convention across the plant.
Standards & conformity

Stated precisely — because procurement checks.

What our marks mean, in the words that survive an audit.

Performance

Tested to the IS 4894 / ISO 5801 / AMCA 210 method, in-house on our 200 HP VFD rig. Tested-to-method — not AMCA-certified. Fans above the rig's 200 HP are run at derated speed and scaled to the specified duty by the fan laws.

Quality system

ISO 9001:2015 — third-party certified. Our only third-party certification.

CE conformity

Self-declared per 2006/42/EC + 2014/35/EU. A self-declaration, not a notified-body certificate.

ATEX conformity

Self-declared, Zone 2/22, Category 3, per 2014/34/EU, where the area classification calls for it.

Oil & gas duty

Designed and built to API 673 as project-specific scope.

Welding

ASME Sec IX qualified welders + WPS for every joint.

Balance

ISO 21940 — G6.3 minimum, G2.5 / G1.0 on application.

Vibration

ISO 14694 fan-specific limits; ISO 20816 general evaluation method.

Questions engineers ask

Chemical & petrochemical fan questions, answered straight.

Can you supply the fans across the whole chemical plant, or only one duty?
Across the whole plant. We have delivered 908 chemical & petrochemical fans spanning fired-heater and process-boiler forced and induced draught, corrosive gas exhaust from reactors and vents, hazardous-area and solvent exhaust, FGD and wet-scrubber boosters, hot-gas (>300 °C) process fans, general and dilution ventilation, process- and combustion-air blowers, and dirty-side dust extraction. Each fan is engineered to its own gas chemistry, temperature and area classification — the clean fired-heater FD and the wet corrosive scrubber booster are different machines — but they come from one partner, on one engineering convention across the plant.
Our process gas is corrosive — acid vapour and chlorides. What metallurgy do you use?
We size the metallurgy to your gas analysis, not a default. On corrosive duty we select from Corten, 316L, or a higher alloy on the wetted surfaces, with coating or FRP-lining options where they suit the gas better. The right answer depends on your acid vapour, chloride content, moisture and temperature, so we choose the material and the corrosion allowance from your figures. Send us the gas analysis and the operating point and we specify the alloy on the GA drawing you sign off before we cut metal.
The area is classified hazardous. How do you build the fan for ATEX?
Where the area is classified we build the fan to an ATEX construction for the zone — non-sparking wheel-to-casing clearances and material pairing, a bonded and earthed rotor, and bearings kept outside the airstream and monitored, built spark-safe to the gas group and temperature class your area classification specifies, to keep internal surfaces below that stated temperature class. To be precise: ATEX Zone 2/22 is self-declared per 2014/34/EU (Category 3) — it is a self-declaration of conformity for the zone you specify, not a third-party certification, and we build to the equipment category your area classification calls for. Tell us the zone, gas group and temperature class and we engineer to it.
We have a wet FGD or scrubber booster at the acid dew point. What do you do?
The scrubber booster sees the most aggressive condensate in the plant — saturated gas at the acid dew point, typically 120 to 150 °C. We keep the casing wall above dew point with insulation and heat tracing, select corrosion-resistant metallurgy on the wetted surfaces (316L, Corten or higher alloys on request), and add drains at the low points so condensate has nowhere to sit. The dew-point margin and the alloy are sized to your SO₂/SO₃, chloride and moisture, so we engineer it to your gas, not a default.
Can you build to API 673 and match our existing fan's duty and footprint?
Yes on both. We design and build to API 673 for oil-and-gas and petrochemical duty as project-specific scope (allow 5 to 7 working days for the offer). And we reverse-engineer to an existing fan's duty point (flow, static pressure, gas temperature, density and chemistry), bearing centres, inlet/outlet orientation and foundation bolt pattern so the unit drops onto the existing base and ducting — whether it is a fired-heater FD, a corrosive exhaust, a scrubber booster or a process-air blower. Made to your installation, not a nearest-catalogue substitute. Send the old GA, the nameplate, the gas analysis and a curve if you have one, and we match it.
Do you performance-test the fans, and what about AMCA, CE, ATEX and quality certification?
Every fan is performance-tested in-house to the IS 4894 / ISO 5801 / AMCA 210 method on our 200 HP VFD test rig, and dynamically balanced to ISO 21940 G6.3 as standard (G2.5 / G1.0 on application). Fans above the rig's 200 HP are run at derated speed and scaled to the specified duty by the fan laws. Because the rig runs cold air, hot or process-gas operation is extrapolated by fan-law correction for density. To be precise: that in-house testing is to the IS 4894 / ISO 5801 / AMCA 210 method, not AMCA-certified; CE is self-declared per 2006/42/EC and 2014/35/EU, and ATEX Zone 2/22 is self-declared per 2014/34/EU (Category 3) where the area classification calls for it — those are self-declarations of conformity, not third-party certifications. Our only third-party certification is ISO 9001:2015.
Across the range

Where Chemicals & Petrochemicals fits — the fans we deploy, the duties we run, and adjacent industries.

The same engineering, viewed three ways — by fan family, by duty, and by industry. Follow the cross-references.

Take it further

Specs an engineer can use — not a brochure.

Ready to quote?

Send us the duty point. We'll quote in 3 to 5 working days.*

Flow, static, gas temperature, application — or attach a spec, GA drawing or a multi-fan schedule. Engineer to engineer.

Get a quote → Email the desk

ISO 9001:2015 quality system · performance-tested to IS 4894 / ISO 5801 / AMCA 210 method · witnessed FAT on request.

*For our standard range. ATEX and special projects need 5 to 7 working days.

Need this fan for your duty? We quote in 3 to 5 working days, 5 to 7 working days for ATEX and special projects.Get a quote →